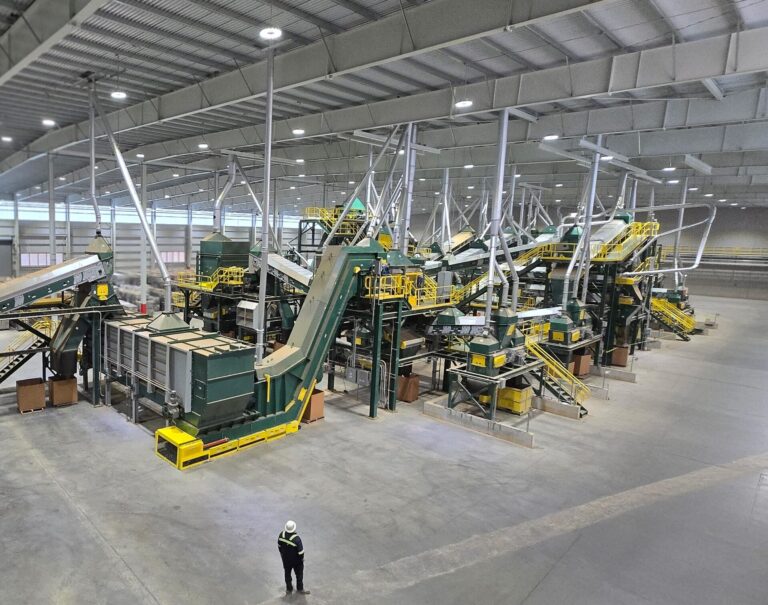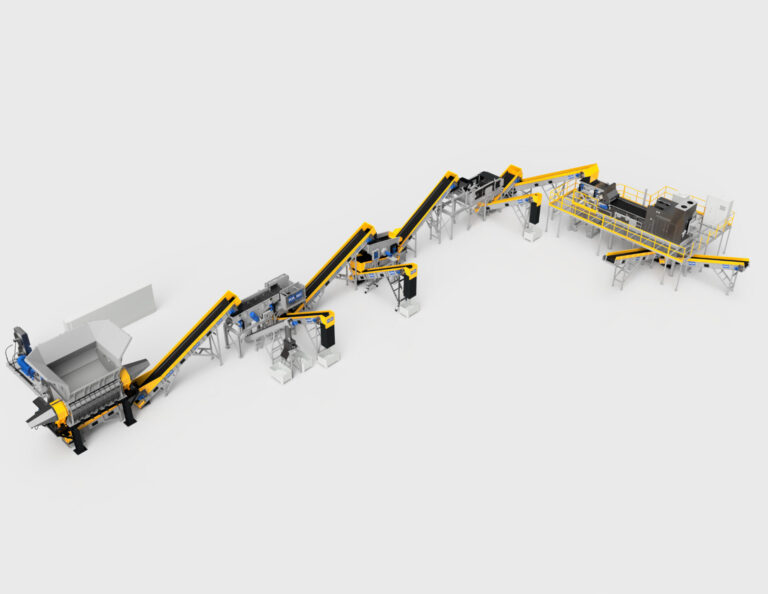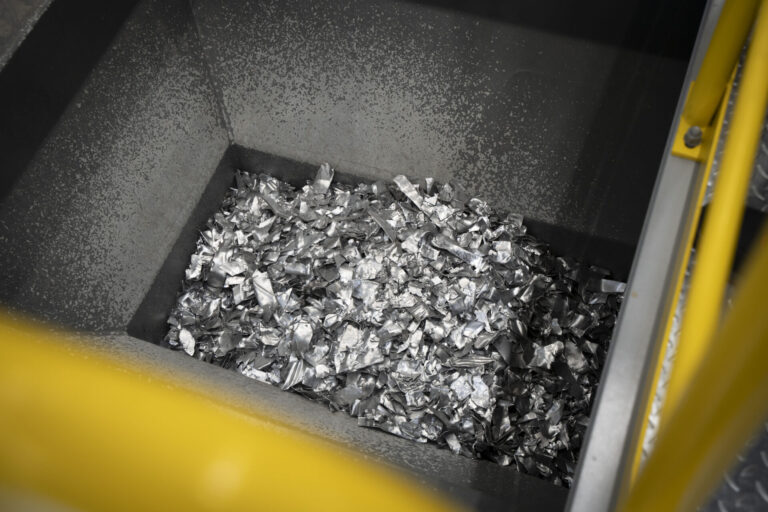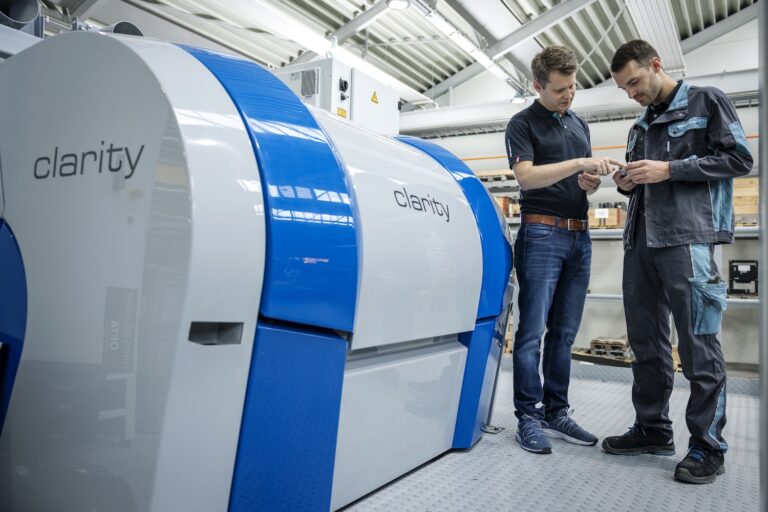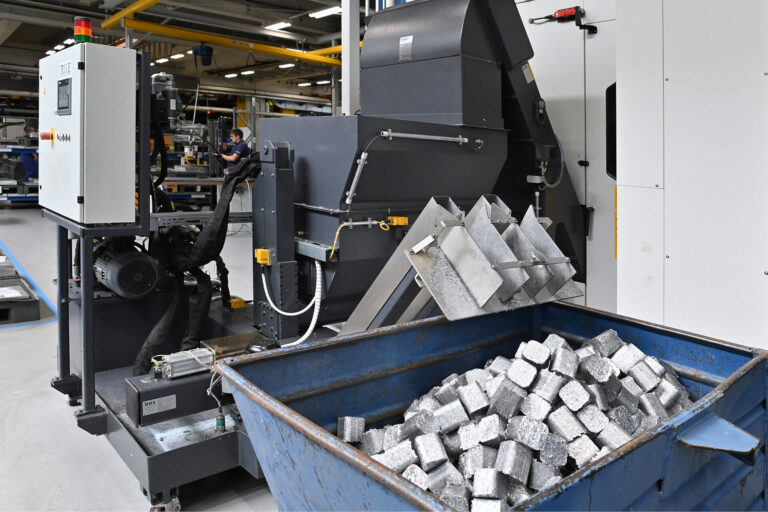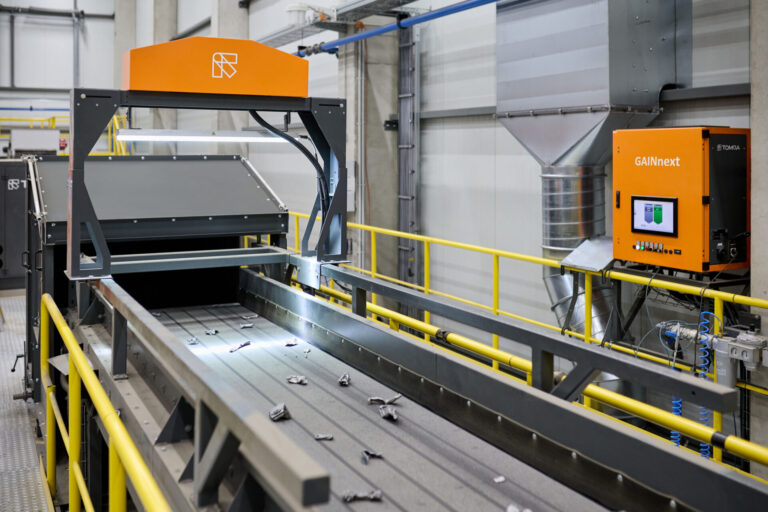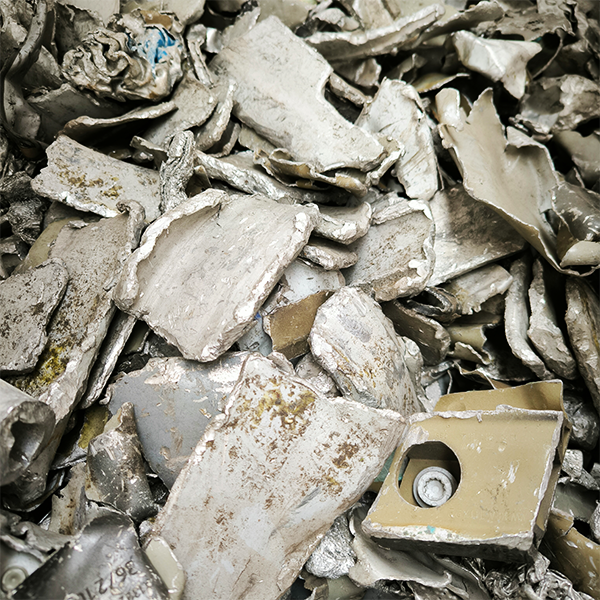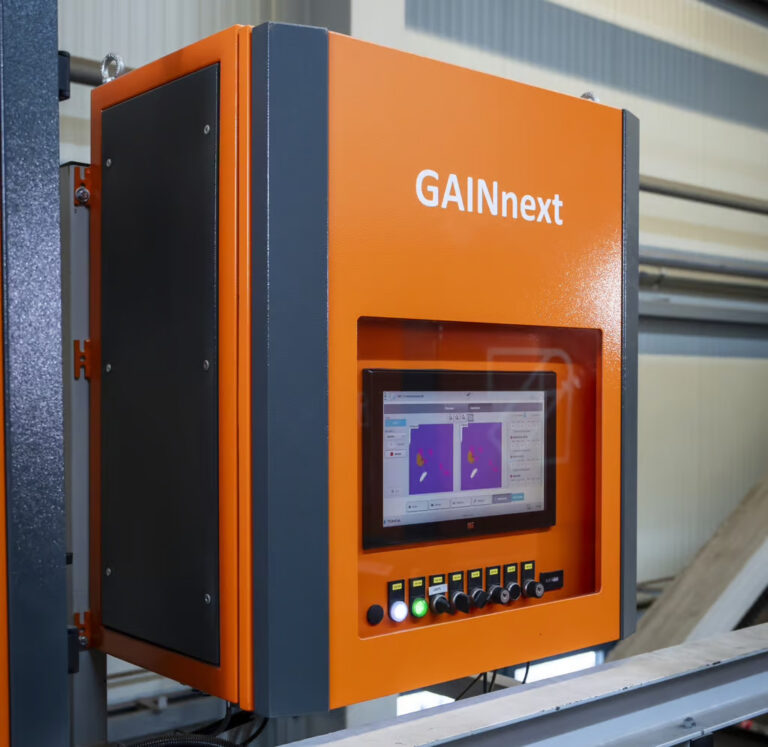
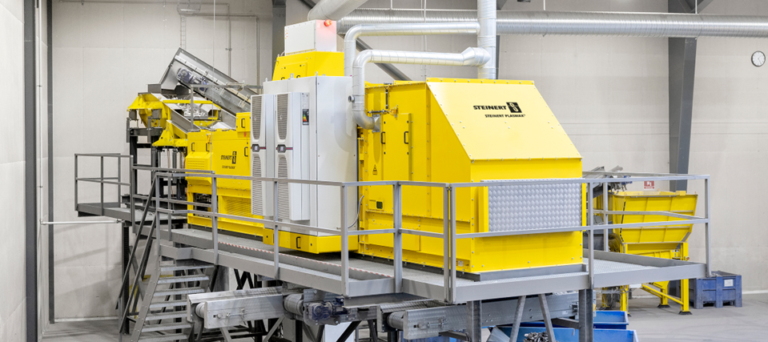
Redefining the State of the Art in Aluminium Recycling, again.
Smaller grain sizes, smarter separation: At ALUMINIUM in Düsseldorf, STEINERT presents technological advances in LIBS and X-ray sorting.

Market
Aluminum is one of the world’s most widely used and highly recycled metals, valued for its durability, versatility, and sustainability. Aluminum recycling involves the collection, sorting, and reprocessing of aluminum scrap so it can be reused in new products without?
Latest in this market
Smaller grain sizes, smarter separation: At ALUMINIUM in Düsseldorf, STEINERT presents technological advances in LIBS and X-ray sorting.
Promoted videos
Ask the Expert
Engineers and product specialists who answer technical questions from readers. The answer comes back to you by e-mail; when we publish it, other readers benefit too.
 Mario VazquezCM Shredders
Mario Vazquez is the Sales & Marketing Director at CM Shredders and a specialist in tire recycling, industrial size reduction, and alternative-fuel? Ask a question
 Dave FlemingSSI Shredding Systems, Inc.
Dave Fleming is the Vice President of Sales and Marketing at SSI Shredding Systems, Inc., bringing over 30 years of dedicated experience? Ask a question
 Daniel WresnikUNTHA shredding technology
Daniel Wresnik, Head of Sales and Business Development BU Waste & Recycling in the DACH region at UNTHA, is a proven expert? Ask a question
 Tom JansenTOMRA Recycling
With more than 20 years of experience in sensor-based sorting technologies, Tom Jansen is VP, Head of Segments at TOMRA Recycling, where? Ask a question
Market & Technology Focus
Every Thursday edition takes one market or technology in depth. These are the editions on this market ? read them online or get the next one by e-mail.
Join 28,000+ engineers, plant managers and technical buyers. Free, twice a week.
What this market covers
Scrap is first sorted by type and alloy, separating used beverage cans from extrusion offcuts, cast automotive parts, and other aluminum grades since each remelts differently. The sorted scrap is then cleaned of coatings, labels, or attached materials where needed and fed into a remelting furnace, where it's melted down and cast into ingots or sows. Those ingots go back into can sheet, extrusion, or casting production, effectively reentering the material supply chain as new aluminum products.
Recycled aluminum can be remelted using roughly five percent of the energy required to produce primary aluminum from bauxite ore, since it skips the extremely energy-intensive electrolytic reduction step of virgin production. Aluminum also retains its properties indefinitely through repeated remelting, meaning a can or extrusion piece can be recycled again and again without degrading in quality. That combination of high recovery value and low reprocessing energy makes aluminum one of the most economically attractive materials in the entire scrap industry.
Used beverage cans, known as UBCs, are graded separately from other scrap because their thin-gauge sheet alloy and consistent composition make them ideal for closed-loop can production. Extrusion scrap, typically from window frames, door frames, and other structural shapes, comes from a different alloy family better suited to extruded products, while cast scrap from automotive wheels and engine parts contains higher silicon content typical of casting alloys. Keeping these grades separate matters because mixing alloys can produce a remelted product that doesn't meet the specifications needed for its intended end use.
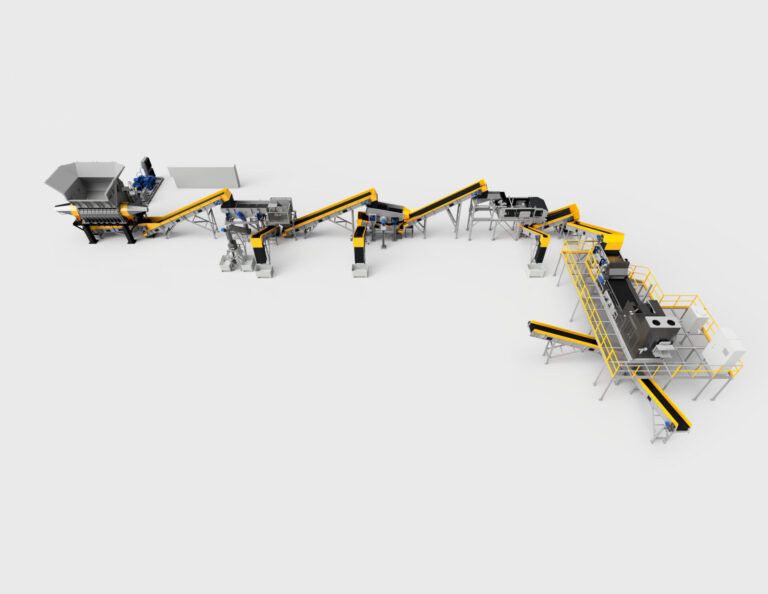
Eddy current separators are the workhorse technology for pulling aluminum out of a mixed waste stream, using a rapidly rotating magnetic field to induce currents in the aluminum that repel it away from non-metallic and ferrous material. Shredders reduce scrap to a manageable size beforehand, and sensor-based sorting systems using X-ray transmission or laser-induced breakdown spectroscopy are increasingly used to distinguish aluminum alloys from one another and from other non-ferrous metals like copper and zinc. These systems allow facilities to process high volumes of mixed scrap while still achieving the alloy purity remelters require.
Producing primary aluminum requires converting bauxite ore into alumina and then using an electrolytic process to extract the metal, a sequence that is extremely electricity-intensive. Remelting recycled aluminum bypasses both of those steps entirely, cutting energy use by roughly ninety percent compared to starting from raw ore. This energy savings is a major reason recycled aluminum commands strong scrap prices and why can-to-can recycling programs are considered some of the most sustainable material loops in packaging.
Coatings, paint, lacquer, and plastic laminates on aluminum products, like the printed exterior of a beverage can or coated siding, need to be burned off or otherwise removed during processing, which adds cost and can generate emissions that require treatment. Mixing incompatible alloys is another major issue, since different aluminum alloys have different alloying elements like magnesium, silicon, or copper, and blending them without control can produce a remelted batch that fails to meet specification. Attached steel fasteners or other metals in composite assemblies also need to be separated out, typically through magnetic separation, before the aluminum fraction is clean enough for high-grade remelting.
Closed-loop can-to-can recycling refers to collecting used beverage cans, remelting them, and rolling the resulting metal back into new can sheet for beverage cans, keeping the material in the same product category rather than downcycling it into a lower-value application. Because UBCs are a relatively consistent alloy, they're well suited to this tight loop, and a significant share of new cans produced today already contain substantial recycled content. Some programs can take a can from recycling bin back to store shelf in as little as sixty days, which is often cited as a benchmark for how fast the loop can turn.
Not entirely — composite materials like aluminum-plastic laminates used in some packaging or aluminum bonded to other metals in automotive or aerospace assemblies require additional separation steps that add cost and can reduce recovery yield. Heavily painted or coated scrap, such as aluminum siding or automotive body panels, needs de-coating before remelting to avoid contaminating the melt and generating excess emissions. Very fine aluminum scrap like machining turnings and fines can also oxidize quickly and is harder to recover efficiently compared to bulkier scrap forms like cans or extrusions.
The scrap industry relies heavily on grading specifications published by organizations like the Institute of Scrap Recycling Industries, which define standardized categories for different aluminum scrap types based on alloy, form, and contamination level. These specifications let buyers and sellers transact on well-understood terms across the global scrap trade, since a remelter needs to know exactly what alloy family and purity level they're purchasing. Environmental regulations, such as air emissions permits for de-coating and remelting furnaces, also shape how processors operate within their local jurisdictions.
Sensor-based sorting technology is improving how precisely mixed aluminum scrap can be separated by alloy, which helps processors recover higher-value grades from streams that used to be downcycled into lower-grade applications. Growing demand for low-carbon aluminum, driven partly by automakers and beverage companies seeking to cut their supply chain emissions, is pushing more investment into recycled content and cleaner remelting operations. The expansion of electric vehicles, which use more aluminum than conventional cars for weight reduction, is also expected to increase future scrap volumes as those vehicles eventually reach end of life.