Incineration, pyrolysis, gasification and drying recover energy and materials from waste that cannot be recycled mechanically. This zone covers thermal processing technology, emission control and the plants that run it.
Klean Industries Inc ("Klean"), a leading equipment provider that owns a commercialized portfolio of intellectual properties and know-how focusing on the recovery of clean energy and resources from…
Thermal Waste Treatment: how it works, key numbers and troubleshooting
Fundamentals
What thermal treatment does
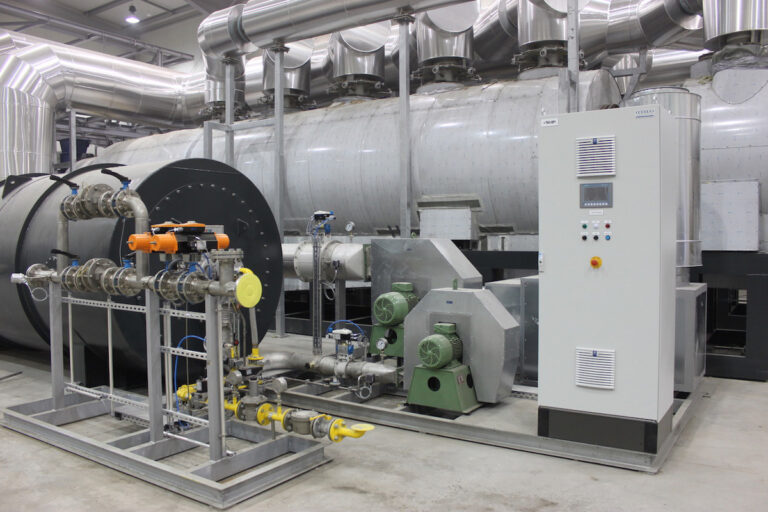
Thermal treatment recovers energy or materials from waste that cannot be recycled mechanically, and reduces its volume and hazard. Incineration burns waste with excess air and recovers heat as steam or power; gasification converts it with limited oxygen into a syngas; pyrolysis heats it without oxygen into oil, gas and char; drying removes water from sludges and organics before further processing. Each route has a different feed requirement, product and emission profile.
Incineration and energy from waste
Grate furnaces take unsorted municipal and commercial waste as received; fluidised-bed furnaces need a prepared, shredded feed and burn at lower temperatures with better control; rotary kilns handle hazardous and liquid waste. The boiler recovers heat for electricity, district heating or process steam; the flue-gas train removes acid gases, dust, heavy metals, dioxins and nitrogen oxides to the emission limits; bottom ash is treated to recover metals and produce aggregate.
Pyrolysis and gasification
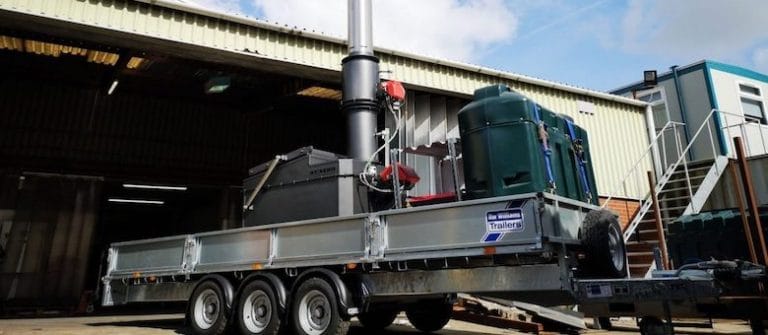
These processes aim at chemicals and fuels rather than heat: pyrolysis oil from plastics and tyres, syngas from wood and refuse-derived fuel, char from biomass. They are sensitive to feed quality — moisture, chlorine, inert content, particle size — and most failed plants failed on feed preparation and on the cleaning of the product gas or oil, not on the reactor. Tyre pyrolysis and chemical recycling of mixed plastics are the growth areas.
Drying and pre-treatment
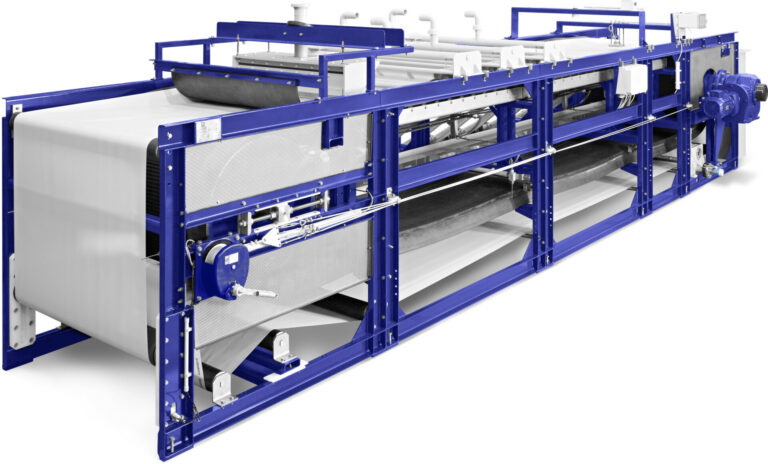
Sludge, organics and wet fractions must be dried before they can be burned efficiently or processed further. Belt, drum and contact dryers use waste heat or flue gas; the exhaust needs odour and dust treatment. Refuse-derived fuel (RDF) and solid recovered fuel (SRF) production — shredding, sorting, drying, pelletising — turns mixed waste into a specified fuel for cement kilns and industrial boilers.
Emissions, residues and permits
Emission limits (dust, HCl, SO2, NOx, dioxins, mercury) drive the design and the operating cost of every thermal plant; continuous emission monitoring is mandatory. Residues — bottom ash, fly ash, flue-gas cleaning residues — need treatment and a disposal or recovery route. The permit sets what can be accepted, at which rate, and what must be measured; acceptance control at the gate is the first line of defence.
Key parameters
Parameter
Typical range
Rule of thumb
Grate incinerator temperature
850–1,100 °C; flue gas ≥ 850 °C for 2 s
The 2-second rule is the legal minimum for destroying organics
Lower heating value of feed
Municipal waste 8–12 MJ/kg; RDF/SRF 12–20 MJ/kg
Below ~6 MJ/kg support fuel is needed
Energy recovery
Electricity 20–25 % of input; combined heat and power up to 80 %
Heat off-take decides the economics more than the boiler
Pyrolysis temperature
400–600 °C plastics and tyres; 500–800 °C biomass
Temperature and residence time set the oil-gas-char split
Gasification temperature
800–1,200 °C; higher for slagging
Tar in the syngas is the classic operating problem
Feed moisture for combustion
< 40–50 % for self-sustaining burn
Drying with waste heat pays back quickly
Bottom ash
20–25 % of input by mass; 5–10 % of volume
Metals recovery from bottom ash is a revenue stream
Engineers and product specialists who answer technical questions from readers. The answer comes back to you by e-mail; when we publish it, other readers benefit too.
No field expert for this zone yet — your question still reaches our editors.
Incineration is the mature route for mixed waste: it accepts almost anything, recovers heat and power reliably and has a proven emission train. Gasification suits prepared, uniform feeds where a syngas has a use nearby. Pyrolysis aims at oils and chemicals from specific streams — tyres, mixed plastics, biomass — and depends on strict feed preparation. For most municipal waste the answer is still incineration; for sorted plastics and tyres the newer routes are becoming competitive.
What feed quality does a pyrolysis plant need?
Dry (usually below 10 % moisture), low in chlorine (PVC out), low in inerts and metals, and shredded to a consistent size. Most plants that underperformed did so because the feed was dirtier and more variable than the design assumed; the sorting and drying steps before the reactor deserve as much attention as the reactor itself.
How is energy recovered from waste?
The furnace heats a boiler that raises steam; the steam drives a turbine for electricity and, in combined heat and power plants, feeds district heating or industrial process heat. Electricity alone recovers 20–25 % of the waste's energy; with a heat off-take total efficiency reaches 70–80 %. The heat customer is the key to the economics.
What is RDF or SRF, and who uses it?
Refuse-derived fuel is shredded, dried and sorted mixed waste with a defined heating value; solid recovered fuel is the standardised version (EN ISO 21640 classes). Cement kilns, industrial boilers and dedicated power plants burn it as a coal substitute. Producing it requires shredding, sorting, drying and often pelletising — a plant in itself.
How are emissions controlled?
A chain of steps after the boiler: dust removal (electrostatic precipitator, fabric filter), acid gas removal (dry, semi-dry or wet scrubbing with lime or sodium bicarbonate), activated carbon for dioxins and mercury, and selective catalytic or non-catalytic reduction for NOx. Continuous emission monitoring reports every value to the authority; the flue-gas train is a large share of both capital and operating cost.
What happens to the ash?
Bottom ash, about a quarter of the input mass, is cooled, aged, screened and stripped of ferrous and non-ferrous metals — a valuable recovery — and the mineral fraction is used as aggregate where regulations allow. Fly ash and flue-gas cleaning residues are hazardous and go to treatment or secure landfill.
Why dry sludge before thermal treatment?
Water carries no energy but takes energy to evaporate: a sludge at 75 % moisture cannot burn on its own. Drying it to 30–40 % with waste heat or flue gas makes it a fuel, reduces the mass to transport and stabilises it. The dryer's exhaust needs odour and dust treatment, and the dried product can self-heat in storage.
What is the difference between this Technology Zone and the Equipment Guide?
The zone is the editorial side: news, case studies, videos, newsletter editions and field experts. The Equipment Guide is the directory side: equipment types and the manufacturers that build them. This page links to its Equipment Guide category and back.
How do I find a manufacturer of thermal waste treatment equipment?
Open the Equipment Guide category for this zone, pick an equipment type and open a manufacturer profile. Partner profiles carry direct contact details; other listings link to the company website.
Can I ask a technical question before I buy?
Yes. Ask the Expert puts your question to a field expert in this zone. The answer comes back to you by e-mail; when we publish it, other readers benefit too.
Your company in this zone?
A basic listing in the Equipment Guide is free. Enhanced and Partner listings add products, videos, an expert profile and a place in the Weekly E-Update.
To provide the best experiences, we use technologies like cookies to store and/or access device information. Consenting to these technologies will allow us to process data such as browsing behavior or unique IDs on this site. Not consenting or withdrawing consent, may adversely affect certain features and functions.
Functional
Always active
The technical storage or access is strictly necessary for the legitimate purpose of enabling the use of a specific service explicitly requested by the subscriber or user, or for the sole purpose of carrying out the transmission of a communication over an electronic communications network.
Preferences
The technical storage or access is necessary for the legitimate purpose of storing preferences that are not requested by the subscriber or user.
Statistics
The technical storage or access that is used exclusively for statistical purposes.The technical storage or access that is used exclusively for anonymous statistical purposes. Without a subpoena, voluntary compliance on the part of your Internet Service Provider, or additional records from a third party, information stored or retrieved for this purpose alone cannot usually be used to identify you.
Marketing
The technical storage or access is required to create user profiles to send advertising, or to track the user on a website or across several websites for similar marketing purposes.
Get compact market and technology updates twice a week — with editorial insights and key industry news delivered straight to your inbox. No spam, only practical insights for recycling professionals.
Tuesday: Weekly E-Update (5-minute summary)
Thursday: Market/Technology Focus (in-depth case)
Independent editorial selection — no sales pitches